Alright, let’s cut to the chase—if you’re knee-deep in industrial equipment, agricultural machinery, or even commercial transport setups, you’ve probably stared at a chain aisle and thought: single-strand vs. multi-strand driving chain. I’ve been on the supplier side for 8 years now, so let’s keep this real, no tech jargon that makes your eyes glaze over. Let’s break down exactly when you should grab a single-strand driving chain, based on the stuff my team’s seen every single day. Driving Chain
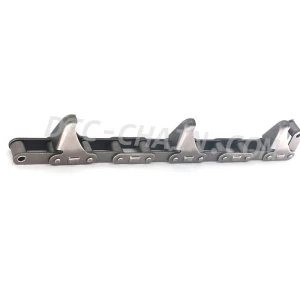
First off, let’s get one thing straight: I’m not here to sell you a $10k chain when you need a $500 one. My job is to make your operation run smoother, not pad my bottom line. So if you’re wondering if single-strand is your call, let’s start with the low-hanging fruit—load size. Wait, not just load size, but consistent load. Like, if your machine is hauling a steady, moderate load, not a fluctuating, “I don’t know if this thing will snap today” load? That’s where single-strand shines. Let’s take an example we deal with all the time: a mid-sized farm’s hay baler. A baler isn’t yanking 5 tons of hay one minute and zero the next; it’s a steady pull of, say, 800-1,200 lbs. My team’s been supplying those farmers with single-strand driving chains for years, and I haven’t gotten a single panicked call from a baler chain snapping mid-harvest. Compare that to a multi-strand chain—those are built for heavy, variable loads, like a construction crane that’s lifting steel one minute and air the next. If you tried to put a multi-strand on that baler, you’d be wasting money, plain and simple.
Next up: space constraints. This is a big one that most first-timers miss. Let’s say you’ve got a tiny gearbox housing, or a narrow conveyor tunnel, or a machine where every inch counts. Multi-strand chains are thicker, right? They need room for all those extra strands to fit, which means you either have to modify your machine (cost you time and cash) or squeeze it in and watch it rub, which leads to wear and early failure. I’ve had a customer come to me last month—small food processing plant, their tiny dough conveyor kept breaking chains. They’d been using multi-strand because their old contractor said “bigger is better.” Turns out, their conveyor housing was only 1.2 inches wide, and a multi-strand was 1.4 inches, so it was scraping the sides every time it ran. We swapped in a single-strand driving chain rated for their exact load, and they texted me two days later saying it’s been running 24/7 without a hiccup. That’s the kind of win we care about.
Then there’s speed and efficiency. Wait, I don’t mean “go fast”—I mean operational speed. Single-strand chains are lighter, period. Less weight means less friction, less energy used to get the chain moving and keep it going. If you’re running a line that’s moving parts or product at a consistent clip, that lighter chain translates to lower utility bills, less strain on your motor, and less wear on other parts of your machine. My team did a test last quarter with a manufacturing client who was using a heavy multi-strand chain on their bottle capping line. They were paying $1,200 a month in electricity for that line. We switched them to a matching single-strand, same load rating, and their monthly electric bill dropped $180. That’s not pocket change—that’s a new set of filters for their equipment, or a bonus for their line workers. The kicker? The single-strand chain cost them 15% less upfront than the multi-strand. No brainer, right?
Wait, let’s talk about maintenance and repair. Let’s be real—no one wants to stop their production line to fix a chain. Single-strand chains are way easier to service. They’re simpler to adjust tension on, simpler to inspect for wear (just look at one side, not three or four), and if you need a replacement link, you don’t have to mess with aligning multiple strands. I had a guy come in last week from a packaging plant, his multi-strand chain broke on their shipping line overnight, and he had to wait 3 hours for a custom replacement because the strands were misaligned when he ordered. We kept a single-strand driving chain in stock in his exact size, and he was back up in 20 minutes. For small operations, or operations where downtime costs you thousands an hour, that’s huge.
But hold up—this isn’t a one-size-fits-all, so let’s talk about the times you don’t use single-strand, to make sure I’m not steering you wrong. If your load is over 2,000 lbs, fluctuating like crazy, or if you need extra strength for high-impact stuff—like a concrete mixer that’s slamming material around—single-strand might not cut it. Also, if you’re running a machine that requires a lot of torque, like a heavy-duty excavator’s drive system, multi-strand is the way to go. But that’s the thing—we’re not here to force single-strand down your throat. We just want to make sure you know when it’s the right call.
Let me throw in a real horror story from a few years back. A construction company reached out to me, swearing single-strand was garbage. They’d put single-strand driving chains on their excavator’s conveyor belt, thinking it was all they needed, and within a week, the chain snapped, damaging the conveyor frame and delaying their project by 2 days. I looked at their specs—they were hauling 3,000 lbs of rock per load, fluctuating non-stop. That’s a job for multi-strand, not single-strand. We fixed them up with the right chains, and they’ve been a repeat customer ever since. So the key here is matching the chain to your specific use case, not what some guy at a trade show told you.
Another point: cost. I mentioned this earlier, but it’s worth repeating. Single-strand driving chains are cheaper upfront, easier to maintain, and last just as long as multi-strand when used for the right job. Let’s do quick math: a multi-strand chain for a mid-sized conveyor is $1,800. A single-strand rated for the same load is $1,200. If you go with multi-strand when you don’t need it, you’re throwing $600 away right off the bat. Plus, the maintenance costs are lower with single-strand—less parts to replace, less labor for repairs. That adds up over time.
Wait, what about corrosion resistance? A lot of our customers in food processing, marine, or outdoor agriculture care about that. Single-strand chains can be sourced with the same corrosion-resistant coatings (stainless steel, zinc plating) as multi-strand, but again, thinner, so the coating is more uniform, and it’s easier to clean. I had a seafood processing plant client last year—their multi-strand chains were getting gunked up with fish residue in the gaps between strands, and they couldn’t get it out, leading to premature rust. We switched them to single-strand stainless steel driving chains, and cleaning took 10 minutes instead of an hour per line. No more rust, no more chain failures.
Let’s wrap this up with a quick checklist, so you don’t have to remember all this:
- Is your load steady, under 2,000 lbs, and not highly variable? → Single-strand is a solid pick.
- Do you have tight space constraints in your machine’s housing? → Single-strand, no question.
- Are you looking to cut energy costs and maintenance time? → Single-strand will help with both.
- Wait, is your load over 2,000 lbs, fluctuating heavily, or high-impact? → Skip single-strand, go multi-strand.
- Do you need ultra-fast, easy repairs to avoid downtime? → Single-strand is way easier to service quickly.

At the end of the day, my team’s job isn’t to sell every customer a single-strand chain. It’s to help you pick the right chain for your operation. If you’re still on the fence, whether you’re a small farm, a manufacturing shop, or a logistics company, don’t guess—reach out, tell me your machine specs, load requirements, and what’s been giving you trouble. We’ll walk through it with you, no sales pressure, no fancy jargon, just real advice from people who deal with this every day. Let’s get your chain sorted so you can get back to running your business.
Industrial Chains References:
- American Society of Mechanical Engineers. (2021). Standard for Power Transmission Roller Chains, Attachments, and Sprockets. ASME International.
- National Agricultural Machinery Manufacturers Association. (2022). Guide to Chain Selection for Medium-Duty Agricultural Equipment. NAMMA Publications.
- Industrial Supply Association. (2023). Energy Efficiency Benefits of Lightweight Power Transmission Components. ISA Technical Report.
- Food and Drug Administration. (2022). Sanitation Guidelines for Processing Equipment Chains and Conveyors. FDA Food Safety Modernization Act (FSMA) Resources.
- Construction Industry Institute. (2021). Downtime Cost Analysis for Heavy Equipment Components. CII Research Report 375.
Hangzhou Dongteng Industrial Co., Ltd.
As one of the most professional driving chain manufacturers and suppliers in China, we have world-leading production equipment and strong manufacturing capabilities. Please feel free to wholesale high quality driving chain made in China here from our factory. Also, custom service is available.
Address: Jingdong Village, Jingjiang Town, Xiaoshan District, Hangzhou City
E-mail: cocowu@dtc-chain.com
WebSite: https://www.dtc-chains.com/
